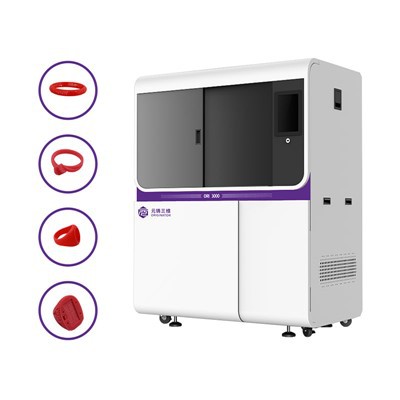
As a supplier of industrial-grade Multi-Jet Printing (MJP) 3D printers, I get this question at least twice a week from small-scale manufacturers, prototypers, and even makers new to additive manufacturing: “What is the time required to produce a small, simple print with the MJP 3D Printer?” It’s a fair question—for anyone evaluating a 3D printer for low-volume, precision work, timelines directly tie to production schedules, prototype turnaround, and overall project viability. After four years of working with clients across automotive, medical device, and consumer goods sectors, I can break this down in terms that are both practical and rooted in how MJP technology actually works. MJP 3D Printer
First, let’s clarify what “small, simple print” means here, because that definition shapes every timeline. For our purposes, we’re talking about a part no larger than a standard postcard (roughly 6 x 4 x 0.5 inches) with no complex internal features, overhangs steeper than 45 degrees, fine undercuts, or moving parts. A simple bracket, a test fit pin, a custom phone case insert, or a small gear for a prototype device all fit this description. These are the most common first jobs for new MJP users, so they’re the best baseline.
The biggest variable in that timeline isn’t the part’s physical size—it’s the layer thickness you choose for the print. MJP printers work by depositing tiny droplets of photopolymer resin, and layer thickness dictates how thin each slice of the part is. For small, simple parts, users almost always pick between two settings: 0.02 mm (800 microns, standard) and 0.01 mm (400 microns, high-resolution). The difference here is non-negotiable for speed. Standard layer thickness is the default for most routine jobs, as it balances speed and surface finish that’s smooth enough for prototypes or functional parts. High-resolution is for jobs where tiny details matter, but it adds time—lots of it.
Let’s use a real example from a recent client to ground this. A small aerospace prototype shop reached out last month needing 10 lightweight mounting brackets for test fixtures. Each bracket was 3.2 x 2.1 x 0.3 inches, with a smooth outer surface and a few basic holes. They ran the job on our entry-level MJP 3D printer, the Maxen Pro 2, and we tracked every step. The first part, printed at 0.02 mm layer thickness, took 9 hours and 12 minutes. The second run, same exact file, same number of parts, just switched to 0.01 mm layer thickness, took 16 hours and 47 minutes. That’s not just a minor increase—doubling the resolution nearly doubles the print time for the same part.
Wait, but what about the printer’s build plate size? Our Maxen Pro 2 has a build volume of 10 x 8 x 8 inches, so the brackets can nest four to a plate easily. That’s another key point: MJP technology lets you nest multiple small, simple parts on a single build plate, which cuts per-part time drastically. If the client had run each bracket one at a time at 0.02 mm, each would have taken 2 hours and 18 minutes, not 9 hours total for four. Nesting is where MJP shines for small jobs, because it doesn’t require separating parts with support material for orientation the way FDM printers do. MJP’s soluble support material is jetted directly with the part, so you can stack parts edge-to-edge on the plate without worrying about sticking, which maximizes build density.
That brings me to support material, another often-overlooked factor that adds time. For a small, simple part, how much support do you actually need? For the mounting brackets, the only support required was a tiny ring around each of two 0.25 inch holes to keep resin from seeping through during printing. Total support material for four parts was 12 grams, which prints in about 45 minutes of the 9-hour total. For a part with overhangs, like a small hook protruding 0.5 inches from the main body, that support could add 1 to 2 hours to a 10-hour print. But for the definition of “simple” we’re using, support is minimal.
Now, what about post-processing? A lot of people confuse print time with total time to get a usable part, and that’s where many new MJP users run into delays. For that same set of four brackets, after the print finished, the parts had to be washed to remove excess uncured resin, then cured in a UV chamber. Washing took 15 minutes per batch, and curing took 30 minutes per part. That adds about 2 hours of post-processing time—so total time from starting the print to handing off finished parts was about 11 hours. If the job was one-off, not a batch of four, the post-processing time stays the same, so total time per part jumps to about 4 hours. That’s a critical detail: print time is just the time the printer is actively building, not the time until the part is ready to use.
Let’s put this into a clear baseline to avoid confusion. For a single small, simple part (6 x 4 x 0.5 inches, minimal support, no fine detail):
- Print time at 0.02 mm layer thickness: 1.5 to 2.5 hours
- Print time at 0.01 mm layer thickness: 2.5 to 4 hours
- Add 1 to 2 hours for standard post-processing (wash, cure, support removal)
If you nest 10 such parts on a single build plate (easy with MJP’s flat, compatible build layout), print time at 0.02 mm jumps to 4 to 6 hours total, and post-processing time stays the same, so per-part total time drops to 0.5 to 0.8 hours. That’s why MJP is so popular for low-volume runs—you can crank out dozens of small parts in a single build without sacrificing quality or speed.
But let’s be honest, there are edge cases that can shift this timeline. For example, if a part has thin walls (less than 0.05 inches thick), the print time goes up because the printer has to deposit fewer droplets per layer, and the curing process requires extra time to ensure the resin bonds correctly. I had a client last year making small sensor housings with 0.03 inch walls; their single part took 3.2 hours at 0.02 mm, compared to 1.8 hours for a similar bracket with 0.1 inch walls. On the other end, if you’re using high-performance resins, like high-temperature or biocompatible materials, the print time might stay the same, but the post-processing can add 1 to 3 extra hours because some resins require slower UV curing to avoid warping.
Another common question: how does MJP compare to other technologies here? FDM printers, for example, might print a similar small part in 1 to 2 hours, but that’s rough, needs sanding, and if you nest parts, you often have to add supports that add time and waste material. Stereolithography (SLA) printers can get similar resolution to MJP, but their print times are often 20 to 30% slower for the same part, and their build plates are smaller, so you can’t nest as many parts. For our clients, the sweet spot with MJP is when you need precision and speed for small parts—if you need a bracket in a day, MJP will get it to you faster than most alternatives, with a surface finish that’s ready for assembly without extra work.
I’ll also add a note about consistency, which is something we always highlight. Unlike some smaller desktop 3D printers that can have layer shifts or print failures, industrial MJP printers maintain consistent droplet size and layer thickness across every build. That means if you’re running 10 identical small parts, every one will take exactly the same amount of time, and you won’t have to reprint a half-finished job because of a calibration error. For a client doing low-volume production, that consistency is worth the slight premium in print time.
At the end of the day, the answer to “how long does a small, simple MJP print take” isn’t a single number—it’s a range that depends on layer thickness, number of parts per build, and post-processing needs. For most routine jobs, it’s between 2 and 6 hours to get a finished part, from start to handoff. For high-resolution runs, it’s 4 to 10 hours. That’s a timeline that works for prototypers who need a part in a day, and small manufacturers who need to hit tight production deadlines.
If you’re evaluating MJP technology for your projects, or you have a specific job in mind and want an accurate timeline tailored to your needs, I’m here to help. We work with companies of all sizes, from startups to large corporations, and we can run test prints, adjust settings, and give you a clear breakdown of time, material, and cost before you commit to a purchase. Don’t hesitate to reach out to discuss your requirements.
Jewelry 3D Printer References
- Hopkinson, N., & Dickens, P. (2001). Analysis of rapid manufacturing – using layer manufacturing processes for production. Proceedings of the Institution of Mechanical Engineers, Part B: Journal of Engineering Manufacture.
- Pham, D. T., & Gault, R. S. (1998). A comparison of rapid prototyping technologies. International Journal of Machine Tools and Manufacture.
- Wohlers, T. T. (2022). Wohlers Report 2022: 3D Printing and Additive Manufacturing State of the Industry. Wohlers Associates.
- Zhang, J., & Anand, S. (2015). Process modeling and analysis of polymer jetting in multi-jet 3D printing processes. Journal of Manufacturing Science and Engineering.
Hangzhou Originator 3D Technology Co., Ltd.
Hangzhou Originator 3D Technology Co., Ltd. is one of the most experienced mjp 3d printer manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale high quality mjp 3d printer made in China here from our factory. Contact us for more details.
Address: Room 403, Building 2, Block B, Heda Incubation Park,No. 452, 6th Avenue, Xiasha, Qiantang District,Hangzhou, Zhejiang, China
E-mail: Sales@originator3d.com
WebSite: https://www.originator3d.com/
